Choosing a Metal welding technology supplier in China requires more than comparing machine prices. It means checking whether the supplier can deliver stable weld quality, dependable service, and equipment suited to your production line. The market is growing: Grand View Research estimated the global welding products market at USD 20.37 billion in 2023, with continued growth projected through 2030. China also has a large automation base. The International Federation of Robotics reported 276,288 industrial robot installations in China during 2023, representing 51% of global installations.
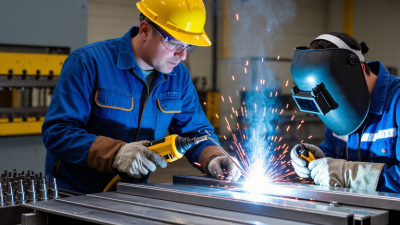
Technology alone does not guarantee a good result. Ask for sample welds using your actual material, thickness, joint design, and production speed. Inspect the bead, penetration, spatter, and consistency across repeated runs. Request details about power sources, process options, control systems, spare parts, training, and response times. A polished demonstration is useful, but not enough. Your own workpiece is the real test.
Professor Sindo Kou, author of Welding Metallurgy, highlights the close relationship between welding conditions and the resulting metal structure. His work offers a useful principle: “The thermal cycle matters.” Treat this as a concise paraphrase of his technical emphasis, not a verbatim quotation. Supplier evaluation also involves judgment. A lower quote may hide service gaps; a famous brand may exceed your needs. Visit the factory where possible, verify references, and record test results. Some details will remain uncertain until installation. That is worth acknowledging. A careful trial can reveal problems before they reach the production floor.
Before contacting a metal welding technology supplier in China, turn the part drawing into clear welding requirements. Name the process you expect, or ask the supplier to recommend one for your joint design. MIG/MAG welding may suit faster work on thicker steel, while TIG can offer closer control on thin stainless steel. Laser and resistance welding may fit specific geometries, but setup needs differ. Details matter.
List every material grade, coating, and thickness range. A 1.2 mm stainless panel behaves differently from a 6 mm carbon-steel bracket. Include joint type, access limits, and production volume. Then state tolerances for bead appearance, distortion, penetration, and final dimensions. Avoid vague terms such as “high precision.” Give measurable limits, such as an allowable gap or dimensional deviation, where your design permits.
Ask how the supplier will verify the process before full production. Request sample welds using your actual material and thickness, then inspect them against agreed criteria. Review procedure records, operator qualifications, inspection methods, and calibration practices. A polished sample is useful, but it does not prove stable output across a production run. It is easy to over-specify tolerances; I would revisit each limit with the engineering team before requesting quotations.
How to Choose Metal Welding Technology Suppliers in China?
Check Welding Quality Systems Against ISO 3834 Requirements
China produced 1,019.1 million tonnes of crude steel in 2023, according to World Steel in Figures 2024. That scale makes consistent fabrication controls important, but production volume alone says nothing about a supplier’s weld quality. Ask which ISO 3834 requirements the supplier follows. Part 2 sets comprehensive quality requirements for fusion welding; certification should match the work and site you are buying.
Review more than the certificate. Check welding procedure specifications, supporting qualification records, welder qualifications, inspection plans, and material traceability. Ask how the shop controls consumables, equipment calibration, nonconformities, and subcontracted welding. Request a recent job file with identifying details removed, then compare its records with a sample weld and inspection results. Scale is not proof. Paperwork can look tidy while a weld sample tells another story. Confirm the certificate’s scope and validity with its issuing body; ISO 3834 certification does not guarantee every joint is defect-free.
Tips: Visit the production floor if possible. Watch how operators identify materials and record preheat temperatures. Ask who approves procedure changes. A vague answer is worth noting, even if the paperwork appears complete.
| How to Choose Metal Welding Technology Suppliers in China? — Check Welding Quality Systems Against ISO 3834 Requirements | |||
|---|---|---|---|
| Evaluation Area | Relevant Standard or Framework | What to Verify | Evidence to Request / Decision Record |
| Quality level selection | ISO 3834-1; ISO 3834-2, ISO 3834-3, or ISO 3834-4 | Confirm that the supplier’s welding quality requirements match the product’s complexity, intended service, applicable codes, and contract requirements. | Documented rationale identifying the selected ISO 3834 part and the customer or regulatory requirements it addresses. Record: Verified / Gap / Not applicable |
| Contract and technical review | Applicable ISO 3834 part; contract and product requirements | Check that the supplier reviews drawings, materials, welding processes, acceptance criteria, inspection needs, delivery requirements, and any changes before production. | Completed contract or technical review records, approved drawings, and a process for controlling revisions and clarifications. Record: Verified / Gap / Not applicable |
| Welding coordination | ISO 3834; ISO 14731 | Verify that welding coordination responsibilities are assigned to personnel with knowledge and authority appropriate to the work, including oversight of welding procedures, personnel, and production controls. | Named responsibilities, evidence of relevant competence, and access to the person responsible for welding coordination. Record: Verified / Gap / Not applicable |
| Welder and operator qualifications | ISO 3834; applicable qualification standards, such as ISO 9606-1 for steel welders or ISO 14732 for welding operators | Check that qualifications cover the actual process, material group, joint type, position, thickness or diameter range, and other applicable variables. | Current qualification records and a production assignment list linking personnel to the work they perform. Confirm applicable validity and continuity requirements. Record: Verified / Gap / Not applicable |
| Welding procedures | ISO 3834; applicable WPS and WPQR standards, such as ISO 15609 and ISO 15614 | Verify that written welding procedure specifications are available at the work station and are supported by procedure qualification or another permitted qualification route where required. | Approved WPS documents and supporting WPQRs or other applicable qualification evidence, with essential variables covering the production work. Record: Verified / Gap / Not applicable |
| Materials and consumables | Applicable ISO 3834 part; material and consumable specifications | Check receipt, identification, storage, issue, and handling controls for base materials and welding consumables, including any required drying or controlled storage. | Material certificates where specified, receiving records, identification or traceability records, and consumable storage and handling instructions. Record: Verified / Gap / Not applicable |
| Equipment and measuring resources | Applicable ISO 3834 part; equipment and measurement requirements in the contract | Confirm that welding and inspection equipment is suitable for the work, maintained, and checked or calibrated when measurement accuracy affects conformity. | Equipment register, maintenance records, and current calibration or verification records for relevant measuring and monitoring devices. Record: Verified / Gap / Not applicable |
| Production controls and traceability | Applicable ISO 3834 part; project and contract requirements | Review controls for fit-up, joint preparation, preheat, interpass temperature, welding sequence, environmental conditions, and identification of welds or materials where required. | Production instructions, inspection checkpoints, weld maps or equivalent records, and traceability evidence at the level required by the contract. Record: Verified / Gap / Not applicable |
| Inspection and testing | Applicable ISO 3834 part; specified product codes and acceptance criteria | Confirm that inspection before, during, and after welding is planned to the extent required, and that the acceptance criteria are defined by the applicable contract or product standard. | Inspection and test plan, visual inspection records, required NDT reports, and clearly identified acceptance criteria. Verify that NDT personnel qualifications meet the specified requirements. Record: Verified / Gap / Not applicable |
| Nonconformities and corrective action | Applicable ISO 3834 part; project quality requirements | Check how the supplier identifies, controls, evaluates, and documents nonconforming welds, repairs, concessions, and corrective actions. | Nonconformity and repair records, approved repair procedures where required, re-inspection results, and evidence that customer approval is obtained when specified. Record: Verified / Gap / Not applicable |
| Subcontracted welding or inspection | Applicable ISO 3834 part; purchasing and contract requirements | Determine whether any welding, heat treatment, or inspection is subcontracted and how the supplier controls the subcontracted work and remains responsible for conformity. | Subcontractor scope, purchase requirements, qualification or capability checks, and review of relevant inspection and production records. Record: Verified / Gap / Not applicable |
| Records and document retention | Applicable ISO 3834 part; contract and applicable regulations | Confirm that required welding, inspection, qualification, material, and traceability records are retained, retrievable, and protected for the specified period. | Record index or retention procedure and a sample job file demonstrating that required records can be retrieved. Record: Verified / Gap / Not applicable |
When evaluating metal welding technology suppliers in China, ask for the approved welding procedure and its supporting qualification record. ISO 15614 addresses procedure qualification through testing, but the relevant part and test scope matter. Check that the record matches your production process, material group, thickness range, joint type, and welding position. A qualified procedure may not cover every variation in your drawing. Request traceable records, not only a summary sheet, and compare the details with the parts you actually need made.
ISO 9606 concerns welder qualification. Confirm that each assigned welder holds a current qualification for the process and work range involved. Check the certificate details, identification, test position, and continuity records against the applicable standard and project requirements. Paperwork can mislead. Ask the supplier to show how welders are assigned to jobs and how qualifications are monitored. If practical, witness a sample weld or review inspection records linked to a specific production batch. I would still ask questions when documents look complete; a certificate alone does not prove consistent shop-floor practice. A careful cross-check can reveal gaps before they become costly rework.
A supplier’s stated monthly output means little without a product-specific production record. Ask for shipments over the past six months, separated by material, thickness, and welding process. Check whether the figures reflect finished, inspected parts—not theoretical machine capacity. The 2024 workforce study by Deloitte and the Manufacturing Institute projects 3.8 million U.S. manufacturing jobs will be needed by 2033, with 1.9 million potentially unfilled. This is not a China capacity benchmark, but it highlights why staffing, welder qualifications, and shift coverage deserve scrutiny. Ask how output changes when a key operator is absent. Numbers need context.
For lead time, compare purchase-order-to-shipment results across several recent orders, including the median and the slowest cases. Request dated schedules for cutting, welding, inspection, and packing; a single quoted number can hide queue time. For quality, ask for first-pass yield, repair rate, and customer rejection rate, each with its denominator and reporting period. A low defect rate based on a tiny sample proves little. Request anonymized inspection records, such as visual checks and applicable nondestructive testing, and verify that reworked welds remain visible in the data. A polished dashboard can still omit awkward delays or repeat repairs. Cross-check a small sample against shipment and inspection records. It takes time. But it is more dependable than accepting a capacity slide at face value.
How to Choose Metal Welding Technology Suppliers in China?
Confirm Traceability, Inspection Records, and Export Compliance Before Contracting
A supplier’s welding claim matters less than the records behind it. Request a sample traceability pack before signing: material certificates, heat or batch numbers, approved welding procedures, welder qualifications, and inspection results. Check that identifiers match across the certificate, part marking, and packing list. Ask for evidence.
For critical joints, review visual inspection criteria and any required radiographic, ultrasonic, or other non-destructive testing reports. Confirm equipment calibration dates, inspector qualifications, acceptance criteria, and how nonconforming parts are controlled. ISO 3834 and relevant procedure and welder qualification standards can help define expectations, but verify which editions and requirements apply to your project. Paperwork can drift. Even capable factories can miss a link between a batch and a finished assembly, so trace one order end to end.
Export documents deserve the same scrutiny. UNCTAD’s Review of Maritime Transport 2024 reports that over 80% of world merchandise trade by volume moves by sea. Ask the supplier to align product descriptions, quantities, origin details, and package marks across commercial and shipping records. Confirm who prepares each document and who checks tariff classification and destination requirements; responsibilities vary by shipment. A polished PDF is not enough. Compare a draft document set against a real order, then resolve mismatches before production or dispatch.