10 Tips for Manufacturing Workflow Optimization

Manufacturing workflow optimization is no longer limited to faster machines or larger production volumes. It connects planning, materials, operators, quality checks, maintenance, and delivery decisions. A delayed inspection can leave pallets waiting beside a loading bay. A missing component can stop an otherwise healthy assembly line.

Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of surveyed leaders expect smart manufacturing to become a primary competitiveness driver within five years. That expectation is significant, but it is not a guarantee. Rockwell Automation’s 2024 State of Smart Manufacturing Report also highlights continued investment in connected systems, analytics, and automation. However, technology alone rarely fixes unclear responsibilities or inaccurate production data. The process must come first.

This guide presents ten practical tips for improving manufacturing workflows. Each tip focuses on visible operational details, such as queue time, changeover minutes, rework frequency, and machine availability. Industry research from the World Economic Forum’s Global Lighthouse Network shows that leading factories combine digital tools with disciplined process redesign and workforce involvement. The lesson is uncomfortable. Many plants collect more data than they use. Some dashboards look impressive while operators still rely on handwritten notes. Progress may begin with one work cell, one reliable metric, and one honest conversation.

The recommendations are designed for plant managers, operations leaders, engineers, and continuous improvement teams. They support safer, clearer, and more measurable decisions. Results will differ across facilities. That limitation matters. A workflow that succeeds in automotive production may fail in food processing or highly customized manufacturing. Testing, reviewing, and adjusting remain essential.
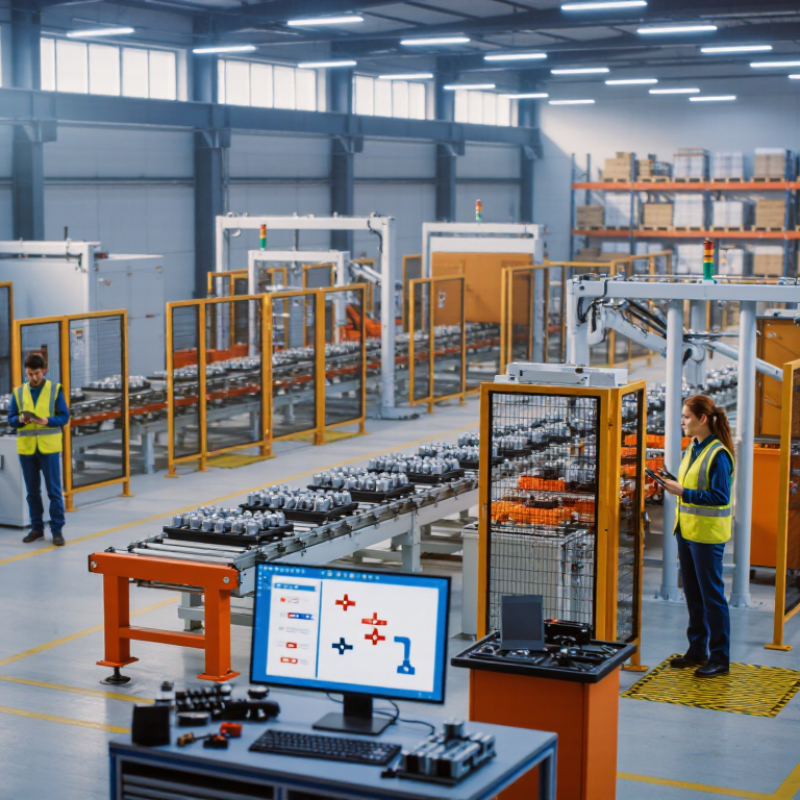
10 Tips for Manufacturing Workflow Optimization

Understanding Manufacturing Workflow Optimization

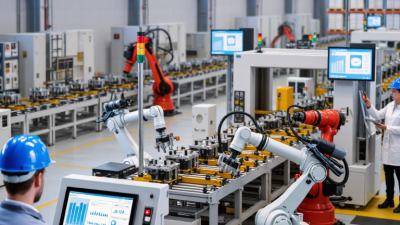
Manufacturing workflow optimization begins with understanding how work actually moves, not how a procedure says it should move. A supervisor can map each step from material receipt to final inspection, recording queue time, processing time, rework, and handoffs. Walk the floor. In one assembly line I reviewed, operators waited beside a test station while completed units accumulated in carts. The bottleneck was not machine speed; it was an unclear inspection schedule.

Reliable analysis uses several weeks of production data, because one busy shift can create a misleading picture. Compare planned cycle times with actual times, then separate equipment downtime from shortages, changeovers, and training gaps. Small details matter. A scan at every transfer may reveal repeated movement that paper records hide. Still, automation should follow understanding; digitizing a confused process only makes confusion faster.

Improvement works best when operators help test the change and define a measurable target. A practical trial might reduce walking distance, place tools within reach, and set a visible response time for maintenance calls. Track throughput, first-pass yield, safety observations, and overtime together. One metric can reward the wrong behavior. Review results after two weeks, ask what failed, and adjust the standard work before expanding it. Some improvements will look inefficient at first, especially when teams are learning a new sequence. That discomfort deserves investigation, not instant rejection.

Mapping Current Processes and Identifying Bottlenecks

A reliable workflow improvement starts with an honest map of the current process. On a recent shop-floor review, the team tracked one order from material release to final inspection. We recorded every handoff, queue, approval, machine stop, and rework loop. A simple wall chart exposed delays that production reports had missed. Operators also explained why certain steps took longer during late shifts.

PROCESS DATA Measure the process as it really operates. Capture cycle time, waiting time, work-in-progress, changeover duration, and defect frequency. Use timestamps from several orders, not one convenient example. The slowest station is not always the true bottleneck. Sometimes upstream batching starves it. Sometimes inspection creates a hidden queue. Look for repeated congestion.

Our first process map was incomplete. We ignored minor material searches because each lasted only a few minutes. Together, they consumed nearly an hour per shift. That finding changed the improvement plan. Validate each suspected bottleneck with operators, supervisors, and maintenance records. Then test one focused change, such as point-of-use materials or smaller production batches. Keep the original measurements for comparison. Resist redesigning the entire workflow at once. Small experiments reveal whether the constraint is real or merely visible.

Standardizing Tasks, Materials, and Production Information

Manufacturing workflow optimization begins with consistent work, materials, and production information. Each task should have one clear method. A workstation card can show required tools, safety checks, torque settings, and inspection points. Keep the language simple. Operators should not search through outdated files during a busy shift. Photos can clarify difficult steps, especially when part orientation matters.

Materials also need a standard flow. Label every container with the item code, lot number, quantity, and storage condition. Use fixed locations for common components. Record damaged packaging immediately. A missing label can stop an entire line. Small details matter. Digital records should match physical stock, including partial boxes and opened containers. This prevents avoidable shortages and incorrect substitutions.

Production information must remain controlled and visible. Set one revision for each instruction, and remove obsolete copies from work areas. Supervisors can review completion data, defect patterns, and changeover times each week. These checks support practical decisions, not assumptions. We once treated a recurring delay as a staffing issue, but the real problem was an unclear inspection step. The revised instruction helped, although the first version was still too technical. Feedback from operators exposed that weakness. Standardization is useful, but it should not become rigid. Review the process when equipment, materials, or customer requirements change.

10 Tips for Manufacturing Workflow Optimization - Standardizing Tasks, Materials, and Production Information
Tip Workflow Area Standardized Practice Key Data to Track Typical Starting Point Practical Improvement Target Recommended Frequency
1 Task Definition Create standardized work instructions with task sequence, cycle time, quality checkpoints, safety requirements, and escalation rules. Standard work coverage, cycle-time variance, training completion, first-pass yield 60% of recurring tasks documented; cycle-time variance of 15% 90%+ task coverage and cycle-time variance below 10% Review monthly and after every process change
2 Material Identification Use consistent part numbers, descriptions, units of measure, storage locations, and revision-controlled material records. Picking errors, material-search time, duplicate records, inventory accuracy Inventory record accuracy of 92%; 8 minutes average search time 98%+ inventory accuracy and search time below 3 minutes Audit weekly; cleanse master data quarterly
3 Production Scheduling Schedule jobs using verified machine capacity, labor availability, material status, setup requirements, and due dates. Schedule adherence, on-time completion, queue time, capacity utilization Schedule adherence of 78%; average queue time of 1.5 days 90%+ schedule adherence and queue time reduced by 20% Update daily; review constraints each shift
4 Changeover Management Separate internal and external setup activities, prepare tools and materials in advance, and use a repeatable changeover checklist. Changeover duration, setup-related downtime, first-piece approval time Average changeover time of 75 minutes 15–30% reduction in average changeover duration Measure every changeover; analyze weekly
5 Quality Control Place inspection points at critical process steps and define acceptance criteria using measurable tolerances and sampling rules. First-pass yield, defect rate, rework hours, inspection completion First-pass yield of 94%; rework equal to 4% of labor hours 97%+ first-pass yield and rework below 2% of labor hours Record each batch or production order
6 Production Information Maintain one controlled source for work orders, drawings, bills of materials, process parameters, and approved revisions. Outdated-document incidents, revision errors, document retrieval time Document retrieval takes 6 minutes on average Retrieval time below 2 minutes and zero unauthorized revisions Verify revision status before each production run
7 Work-in-Process Control Set standard work-in-process limits between process steps and use visual status signals for waiting, blocked, inspected, and released work. WIP quantity, throughput time, blocked orders, aging by process step Average throughput time of 4.0 days 10–20% lower throughput time without increasing defects Monitor every shift; review aging daily
8 Equipment Reliability Standardize preventive-maintenance tasks by asset, operating hours, spare parts, safety checks, and completion criteria. Overall equipment effectiveness, unplanned downtime, mean time between failures, maintenance compliance Preventive-maintenance compliance of 85% 95%+ maintenance compliance and 10% less unplanned downtime Check daily; analyze equipment trends monthly
9 Operator Training Use competency matrices, task qualification records, refresher training, and supervised sign-off for critical operations. Qualified-operator coverage, training hours, safety incidents, process deviations 80% of critical tasks have two qualified operators 100% coverage for critical tasks with at least two qualified operators Update after training and review quarterly
10 Continuous Improvement Use a structured improvement log with problem statement, root cause, countermeasure, owner, due date, and verified result. Action closure rate, recurring issues, improvement lead time, verified savings Action closure rate of 70%; improvement lead time of 45 days 90%+ action closure and improvement lead time below 30 days Review weekly; verify results after implementation

Suggested measurement rule: establish a four-week baseline before changing the process, then compare results using the same definitions, units, production mix, and reporting period.

Applying Automation, Data, and Lean Improvement Methods

Manufacturing workflow optimization improves when teams observe work before changing it. Map each step from material arrival to final inspection. Automate repetitive transfers, data entry, and routine quality checks. Capture cycle time, defects, downtime, and changeover delays. Keep sensors calibrated and records consistent. Establish one shared dashboard for production and maintenance. Ask operators where delays begin. Their experience often reveals hidden friction. Listen closely.

Apply lean methods to remove waiting, excess motion, overproduction, and unnecessary approvals. Test one small change before redesigning an entire line. Digital work instructions can reduce variation during complex assembly. Automation should support judgment, not replace skilled decisions. Add alerts for unusual temperatures, cycle times, or defect rates. Review trends daily. Compare planned output with actual output, then investigate the gap. Use control charts when process stability matters. Protect data quality. A missing timestamp can distort a whole analysis.

Train operators on both the tools and the reasons behind each change. Record who adjusted a setting and why. Standardize successful settings, but leave room for safe improvement. Not every bottleneck needs advanced technology. Sometimes a misplaced container causes more delay than a complex software issue. If automation increases rework, pause the rollout and inspect the workflow again. Recheck assumptions. Review results with the people doing the work. A failed trial still provides useful evidence. Keep it visible.

Measuring Results and Sustaining Workflow Performance

A workflow improves only when its performance is measured against a stable baseline. Record cycle time, queue time, first-pass yield, downtime, and rework for each production cell. Use the same definitions every week, or comparisons become misleading. Numbers expose drift. A practical review may reveal that a ten-minute changeover saves labor but creates longer inspection queues. That trade-off should be recorded, not hidden.

Supervisors should display a simple daily board near the line. It can show target output, actual output, stoppage minutes, and defects by cause. Operators need access to the figures and a safe way to challenge them. Their observations often explain patterns that software misses. Keep it visible. If a measure cannot guide a decision, remove it or redesign it. Too many indicators create reporting work without improving control.

Sustaining gains requires scheduled audits, clear process ownership, and short corrective-action cycles. Recheck the workflow after staffing changes, new materials, or equipment maintenance. A weekly review can assign one owner, one deadline, and one verification method for each gap. Do not celebrate a lower cycle time if safety checks or product quality have weakened. We once treated stable output as success, then found hidden rework downstream. The metric was incomplete. That mistake changed our review method.

Translate