In 2026, Manufacturing process efficiency is not simply about running machines faster. It means producing the right part, at the required quality, with less waiting, scrap, energy, and avoidable downtime. The stakes are substantial: the International Energy Agency reports that industry accounts for about 37% of global energy use. Deloitte’s 2025 Smart Manufacturing Survey found that 92% of surveyed manufacturing executives see smart manufacturing as a key driver of competitiveness over the next three years. Yet sensors alone cannot fix a poorly balanced line. A dashboard cannot explain why a feeder jams every Tuesday or why finished parts wait beside inspection. The floor tells the truth.
Industrial engineer Shigeo Shingo warned, “The most dangerous kind of waste is the waste we do not recognize.” That is a useful warning, not a complete playbook. Start with a value-stream map and reliable baselines for overall equipment effectiveness, first-pass yield, cycle time, and energy per unit. Then address the biggest constraint and check whether changes work for frontline operators. Small, visible tests can expose issues before they become expensive rollouts. Even strong projects can stall when teams optimize a machine but overlook changeovers, quality holds, or operator workload. The numbers matter. So does the work behind them. This guide examines practical ways to reduce losses, strengthen daily problem-solving, and use digital tools with purpose—while recognizing that no single efficiency target fits every plant.
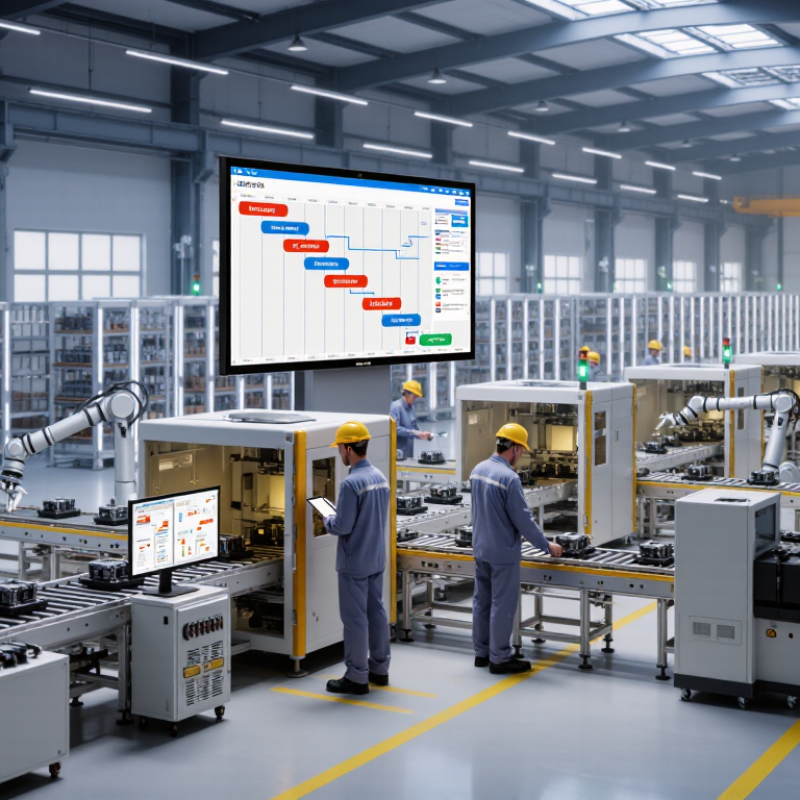
Set a specific efficiency goal before buying equipment or changing a production schedule. For example, target a 10% reduction in unplanned downtime within six months, while keeping defect rates steady. Start with facts. Track availability, cycle time, first-pass yield, scrap, changeover time, and labor hours. Define each metric clearly so supervisors on different shifts record it consistently. A daily log beside the line can reveal whether downtime comes from material shortages, minor stoppages, or maintenance delays.
Build a baseline across several weeks and include every shift and product type. Separate planned maintenance from unexpected stops, and compare similar products to avoid misleading averages. The U.S. Bureau of Labor Statistics reported that manufacturing labor productivity rose 0.3% in 2023, while output fell 0.8% and hours worked fell 1.1%. The figures show why one metric rarely tells the whole story. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of surveyed manufacturing executives expected smart manufacturing to drive competitiveness over the following five years. That supports attention to measurement, not automatic technology spending. Baseline data may be imperfect; note gaps, investigate them, and resist polishing numbers to fit a target.
Improving manufacturing efficiency begins with a clear map of how work actually moves, not how a procedure says it should move. Trace one product from raw material to finished goods. Mark each operation, handoff, queue, inspection, and return for rework. Add the people, machines, and information needed at each step. Walk the floor during different shifts; a neat diagram made in an office can miss a cart waiting beside a busy machine. Details matter.
Record cycle times and waiting times separately. A station with a long cycle time is not always the true bottleneck if it has spare capacity or feeds a buffer. Compare output across several hours or shifts, and note changeovers, small stoppages, and missing materials. Look for queues that keep growing, operators who wait for work, or unfinished parts accumulating before one process. Then check the pattern with operators and production records. Their explanations may challenge the map. Good.
Use a simple current-state map before proposing changes. Estimate where lost time occurs, but label estimates clearly; a few observations can mislead. Review the map after a process or product mix changes. It will never capture every variation, and pretending otherwise can send improvement efforts toward the wrong station.
Illustrative five-day production audit for one product family. Daily averages are shown per eight-hour shift; utilization is calculated as actual output divided by planned capacity. Values are a sample dataset, not measurements from a named facility.
| Process step | Avg. cycle time (min/unit) |
Avg. queue wait (min) |
Queue before step (units) |
Actual output (units/shift) |
Planned capacity (units/shift) |
Capacity utilization | Equipment uptime | Bottleneck signal and improvement opportunity |
|---|---|---|---|---|---|---|---|---|
| Receiving and kitting | 0.8 | 15 | 12 | 480 | 520 | 92.3% | 96% | Small queue and available capacity. Standardize kit locations and replenish to a visual schedule. |
| Machining | 1.6 | 28 | 24 | 410 | 430 | 95.3% | 91% | High utilization and the lowest uptime point to downtime risk. Track stoppage reasons and schedule preventive maintenance. |
| Assembly | 2.1 | 42 | 31 | 365 | 390 | 93.6% | 94% | Work accumulates before assembly. Balance tasks across stations and verify parts are kitted before work starts. |
| Inspection | 1.1 | 61 | 46 | 335 | 340 | 98.5% | 98% | Likely bottleneck: highest utilization, longest queue wait, and lowest planned capacity. Review inspection criteria, reduce repeat checks, and cross-train qualified support. |
| Packing | 1.0 | 18 | 8 | 335 | 420 | 79.8% | 97% | Output matches inspection, indicating downstream constraint rather than packing capacity. Avoid adding packing resources until the upstream constraint is addressed. |
Process-mapping takeaway: Start improvement work at inspection, then remeasure queue size, waiting time, and shift output. Recheck the constraint after each change, as the bottleneck may move to another process step.
Manufacturing efficiency in 2026 starts with finding where time and material are actually lost. Track stoppages, changeovers, rework, and waiting between machines before buying new equipment. A worn conveyor or unreliable sensor may slow an entire line. Replace or upgrade the constraint first, and check that new machinery fits existing workflows and maintenance skills. Small changes matter. Schedule preventive maintenance around real operating conditions, not only a fixed calendar.
Automation works best on repeatable tasks with clear quality checks. Automated loading, inspection, or material movement can reduce delays, while trained operators handle exceptions and adjustments. Keep manual overrides available. Before expanding a system, pilot it on one line and compare cycle time, defect rates, and downtime against a recorded baseline. The results may be less tidy than expected.
Manufacturing data systems should connect machine events, production counts, maintenance records, and quality results with consistent timestamps. A shared dashboard can help supervisors spot recurring pauses, such as a packaging station waiting several minutes for parts. But collecting more data does not guarantee better decisions. Assign owners to key metrics, verify sensor readings, and make sure teams can act on alerts. That takes discipline. Even a useful system can create noise if every small variation triggers an alarm. Define practical thresholds, review them with operators, and revise them when the process changes.
Manufacturing efficiency in 2026 depends on people, materials, and reliable checks working together. Train operators on the specific tasks they perform, not just general procedures. A short practice session at a workstation can reveal gaps that a slide presentation misses. Pair experienced staff with newer employees, and let them explain why a step matters. Skills fade without practice.
Material flow deserves equal attention. Mark clear routes for carts, keep frequently used parts near the point of use, and review inventory levels against actual production schedules. A missing component can idle an entire line. So can a crowded aisle. Simple visual signals help teams spot shortages, but they need regular updates; outdated labels create confusion rather than clarity. Walk the floor during a busy shift and note where workers wait, backtrack, or search.
Quality control works best when checks happen throughout production, not only at the end. Use a consistent inspection method, record recurring defects, and discuss findings with the people doing the work. A small measurement change may prevent a larger batch of rework. Still, more inspections do not automatically mean better quality. Teams should question whether each check catches a meaningful risk. Even a well-designed process can miss something, so review results and adjust carefully.
Illustrative operational targets for strengthening workforce skills, material flow, and quality control.
How to read this: The chart compares example starting measures with proposed 2026 targets. Track certification coverage, material delivery reliability, and first-pass yield regularly to identify improvement opportunities. Figures are illustrative planning targets, not published industry benchmarks.
Manufacturing efficiency improves when teams measure work as it happens, not only at month-end. Choose a few indicators tied to the process: changeover time, first-pass yield, unplanned downtime, and work-in-process. Define each metric clearly, including where the data comes from and who records it. Otherwise, two shifts may report different versions of the same delay. Start small. One packaging line might log stoppages by cause. Those records can reveal brief label-feed jams consuming more time than a weekly machine failure. Review results regularly, using a short shift handoff and a monthly process review. Charts can show trends, but verify unusual spikes with operators before changing settings.
Numbers need context. An output dip might reflect a product mix change, new operator training, or missing material—not poor effort. Ask workers to walk through the steps, then test one adjustment at a time. Record the expected effect, trial period, and actual result. If a revised setup cuts changeover by six minutes but raises defects, the trade-off is not an improvement. Keep useful changes in standard work, and set a review date to check whether gains last. Some experiments will fail. That is useful evidence, though teams should be candid when data is noisy or a target was unrealistic.